How to Choose the Best Milling Tools in 2026
Choosing the best milling tools in 2026 starts with the material, the machine, and the workpiece. A cutter that performs well in aluminum may struggle with hardened steel. Tool geometry, coating, flute count, and cutting-edge strength all affect results. So does the setup. A rigid spindle and secure workholding can make a modest tool perform well; vibration can ruin an expensive one.
Look beyond the catalog. Check the toolmaker’s recommended speeds and feeds, then compare them with your machine’s limits and the job’s requirements. For example, a long-reach end mill may access a deep pocket, but its extra flexibility can increase chatter. A shorter tool is often more stable. Small details matter. Coolant delivery, chip evacuation, and the finish you need should shape your choice, too. Pay attention to actual tool life and surface quality, not just the first cut or the advertised maximum.
This guide explains how to compare milling tools for common materials and operations, from roughing to finishing. It also covers carbide, high-speed steel, coatings, and practical signs of wear. Keep a simple record of tool life and cutting conditions; shop-floor notes can reveal patterns that specifications alone miss. There is no perfect cutter for every job. Even experienced machinists sometimes have to adjust their assumptions after a test cut. A careful choice balances performance, reliability, and cost, while leaving room to learn from the results.
Define the Milling Operation and Required Results
Before selecting a milling tool, describe the operation in physical terms. Are you facing a broad surface, cutting a shoulder, slotting, profiling a contour, or clearing a deep pocket? Each task changes the tool’s reach, cutting-edge engagement, and chip evacuation needs. Record the workpiece material, its hardness if known, and how firmly it can be held. A thin-walled part may vibrate under a cut that feels stable on a solid block. Small details matter.
Next, define a measurable result: target dimensions, tolerance, surface finish, and production quantity. A roughing pass may prioritize material removal, while finishing needs controlled deflection and a clean edge. Check the machine’s spindle range, available power, holder type, and coolant options before comparing tool geometry. Long reach has a cost: added tool length can reduce rigidity. It is easy to focus on feed rate and overlook clamping. That mistake can spoil an otherwise sensible plan. If the drawing leaves room for interpretation, clarify the requirement before choosing flute count, diameter, coating, or edge form. Then review the choice after a test cut; the first estimate may not be right.
How to Choose the Best Milling Tools in 2026 — Define the Milling Operation and Required Results
Define the required surface finish before selecting a milling tool. The chart shows representative Ra targets drawn from commonly used roughness values: roughing prioritizes material removal, while finishing requires a lower Ra. Actual results depend on the workpiece material, tool geometry, cutting conditions, and machine setup.
Identify the Workpiece Material and Cutting Conditions
How to Choose the Best Milling Tools in 2026
Identify the Workpiece Material and Cutting Conditions
Start with the material, not the tool catalog. Aluminum often needs sharp edges and generous chip space because soft chips can cling to the cutter. Stainless steel can work-harden when rubbing replaces cutting, so stable engagement matters. Cast iron is abrasive and produces fine dust; composites may wear edges quickly or splinter at the exit. Small differences matter.
Then look at the actual setup. Note the machine’s available power, spindle speed, workholding, and how far the tool must reach. A long, slender cutter may chatter on a deep pocket, even when its geometry suits the material. Check coolant access and chip evacuation, too. Hot chips trapped in a slot can damage both the finish and the cutting edge.
Match tool material, flute count, edge geometry, and coating to those conditions. More flutes are not automatically better; crowded flutes can leave chips nowhere to go. Avoid choosing cutting data from a chart without checking the machine and setup. Run a measured test cut, listen for vibration, inspect the chips, and check edge wear. Even a sound choice can disappoint when the workpiece varies from the sample. Reassess rather than forcing the original settings.
Match Tool Geometry to the Milling Task
How to Choose the Best Milling Tools in 2026
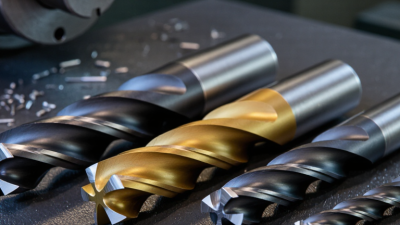
Match the cutter’s geometry to the work, not just the material label. A square-end mill suits flat floors and sharp shoulders, while a ball-nose cutter follows curved surfaces and 3D contours. For corners that chip easily, a corner-radius edge can add strength. Small differences matter. A tool that clears chips poorly may overheat, chatter, or leave a rough wall.
Flute count and helix angle affect chip space, cutting smoothness, and tool pressure. Softer, gummy materials often benefit from open flute space so chips can escape. Harder materials may call for more cutting edges, but only when the machine and setup can handle the load. There is no universal geometry. A long, slender cutter may reach a deep pocket, yet it can deflect under pressure.
Check the operation, too. Slotting, side milling, and finishing place different demands on the cutting edges. Match the tool’s reach and diameter to the pocket, then consider workholding, spindle rigidity, and coolant access. On a real setup, make a cautious test cut and inspect the chips, sound, and surface. I still find that charts cannot fully predict chatter; a small geometry change may help, but it can also shift the problem elsewhere.
Compare Tool Materials, Coatings, and Durability
Material choice sets the limits; coating choice fine-tunes performance. Grand View Research’s 2024 Cutting Tools Market report values the global market at USD 27.7 billion in 2023, reflecting broad demand, not proof that one tool lasts longest. Cemented carbide suits many production milling jobs because it retains hardness at elevated temperatures. High-speed steel is tougher and often tolerates interrupted cuts, but generally loses hardness sooner as heat rises. Ceramic tools can handle high cutting temperatures, yet their brittleness makes setup and workpiece stability critical.
Coatings matter at the cutting edge. TiAlN-based coatings can help resist heat and wear in dry or high-speed cutting; low-friction coatings may help when chip flow and built-up edge are concerns. Conditions decide. A hard coating cannot rescue a tool with excessive runout or poor chip evacuation. Check the maker’s cutting data, then compare tool life on the same material, machine, and finish requirement. Track minutes of productive cutting, not just parts made. One awkward detail: a longer-lasting tool may still cost more if it forces slower feeds. I would test a small batch first, inspect the edge under magnification, and record wear. The market report tracks industry value, not controlled coating trials, so shop tests remain essential.
Verify Machine Compatibility, Availability, and Total Cost
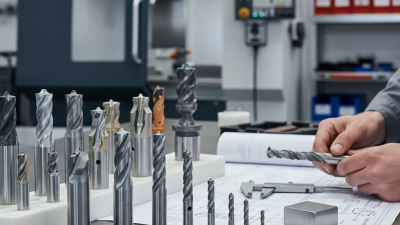
Choosing milling tools in 2026 starts with the machine, not the catalog. Check the spindle interface, maximum speed, power, and tool capacity before comparing cutting edges. A holder that fits physically may still exceed the machine’s speed limit or leave too little clearance. Measure the workpiece and fixture, too; a long tool can collide with a clamp during a deep pass. Small details matter.
Availability deserves equal attention. Confirm whether the tool, compatible holders, and replacement inserts are in stock, and ask about realistic lead times. A cutting tool that saves seconds but arrives weeks late may disrupt a scheduled job. For repeat production, verify that replacement parts will remain accessible. This is easy to overlook when one sample tool performs well. It happened to us on a short-run job.
Compare total cost, not just the listed price. Include holders, inserts, setup time, expected tool life, and scrap risk. Then estimate cost per usable part under your actual cutting conditions. Published life figures may not match your material, coolant, or machine rigidity. Run a controlled trial, record wear and cycle time, and inspect the finished surface. The cheapest option can win, but not always. Keep the results, including the disappointing ones; they make the next selection less of a guess.