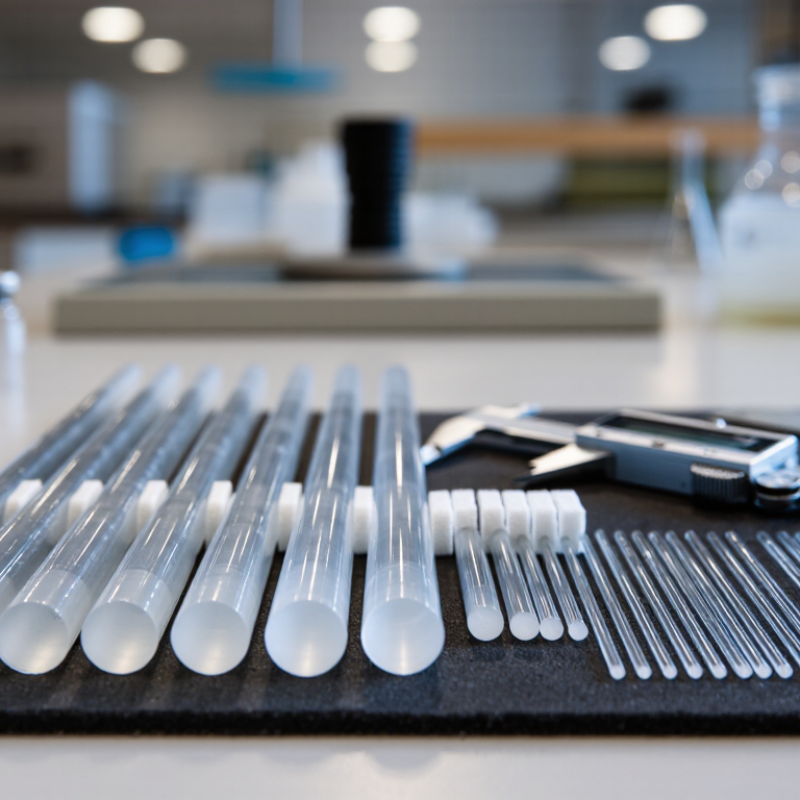
Sourcing Quartz Rods globally in 2026 will require more than comparing prices on supplier websites. Buyers must examine purity, diameter tolerance, surface finish, thermal stability, packaging, and production capacity. A rod that looks clear under warehouse lighting may contain bubbles, stress lines, or microscopic inclusions. These defects can appear later during heating, machining, or laboratory use. Small details matter.
Dr. George H. Rossman, Professor Emeritus of Mineralogy at Caltech, has described quartz as “a mineral that records the conditions of its formation.” That perspective is valuable for procurement teams. Manufacturing history can influence optical transmission, hydroxyl content, and resistance to repeated temperature changes. Reliable suppliers should provide traceable test reports, batch identification, dimensional data, and clear statements about the quartz grade. Certificates alone are not enough. Verify them.
A practical global sourcing process should compare manufacturers from China, Germany, Japan, the United States, and other established production regions. Ask for samples before signing a large contract. Measure them independently. Check how each supplier handles rejected parts, replacement timelines, export documentation, and protective packaging. One overlooked issue is regional communication. A technically strong factory may still create delays through vague drawings or slow feedback.
There is no perfect sourcing route. Freight disruption, currency movement, and changing energy costs can affect final pricing. A cheaper quote may become expensive after inspection and rework. The better decision balances technical evidence, supplier experience, delivery reliability, and transparent communication. Buyers should remain skeptical, even when everything appears convenient. That caution protects performance.
Quartz rods differ by structure, purity, finish, and thermal performance. Fused quartz rods are widely used for laboratory tools, furnace parts, and semiconductor processing equipment. Clear rods transmit ultraviolet and visible light, while opaque rods provide stronger thermal shielding. There are also high-purity grades, commonly described as 4N or 5N. However, grade labels vary between suppliers. Always request a certificate showing measured purity, hydroxyl content, and trace-metal levels.
Application determines the right specification. A rod for a high-temperature tube furnace may need low expansion and excellent thermal-shock resistance. Optical equipment may require controlled transmission, polished surfaces, and tight diameter tolerance. Chemical processing often demands low contamination and strong resistance to acids. Small details matter. A rough end can cause cracks during heating. An incorrect diameter can also increase machining waste.
For global sourcing, prepare a clear drawing with length, diameter, tolerance, surface finish, and packaging requirements. Ask for sample inspection records, dimensional reports, and test methods before placing a large order. Export packaging should protect rods from vibration, moisture, and impact. In practice, the cheapest quotation is not always economical. Freight damage, inconsistent batches, or unclear grade definitions can erase the saving. I would also review production consistency across several lots, not only one impressive sample. Some specifications remain uncertain until real equipment testing begins. That is an uncomfortable, but useful, part of responsible sourcing.
How to Source Quartz Rods Globally in 2026?
Define Technical Requirements and Quality Standards
Global sourcing becomes safer when the quartz rod specification is precise. Start with the application, temperature range, and installation method. State the required length, diameter, tolerance, straightness, and end finish. Include quartz grade, purity, hydroxyl content, and thermal shock resistance. A vague phrase like “high quality” creates disputes later.
Inspect the surface under controlled lighting. Record bubbles, inclusions, scratches, devitrification, and contamination limits. For laboratory or semiconductor use, define surface roughness and dimensional measurement methods. Request a material certificate, batch number, inspection report, and traceability records. The supplier should explain its sampling plan and calibration system. Ask for pre-shipment photographs.
Small details matter.
Use recognized ASTM or ISO methods where applicable, but confirm the exact test version with the supplier. Require samples from the intended production route, not only polished demonstration pieces. Compare samples against a signed reference drawing. A third-party inspection can verify dimensions, packaging, and visible defects before dispatch.
Do not over-specify without evidence. Extremely tight tolerances may increase cost without improving performance. I have seen purchasing teams focus on diameter while ignoring thermal cycling data. That mistake can delay installation. A practical specification should identify critical characteristics, acceptable variation, and the response to nonconforming rods. Keep these decisions in the purchase contract.
| Data Dimension | Technical Requirement | Recommended Acceptance Criteria | Verification Method | Global Sourcing and Quality-Control Notes |
|---|---|---|---|---|
| Material Type | Fused quartz or fused silica rod manufactured from high-purity silica. | Material grade must be stated clearly, including whether the rod is electrically fused, flame fused, or produced by another documented process. | Review material certificate, manufacturing declaration, and traceability records. | Do not compare quotations solely by the term “quartz.” Confirm the material process because impurity levels, bubbles, hydroxyl content, and thermal behavior can differ substantially. |
| Chemical Purity | Impurity profile appropriate for the intended application, especially alkali metals, iron, aluminum, calcium, magnesium, titanium, and copper. | Set numerical limits in the purchase specification; for high-purity optical or semiconductor-related use, limits are commonly defined in parts per million or lower according to the application. | Independent laboratory analysis using ICP-OES, ICP-MS, or an equivalent validated method. | Request a lot-specific certificate rather than a generic brochure value. The required limit should be based on process sensitivity, not only on nominal material grade. |
| Rod Diameter | Round rod diameter selected according to the assembly, machining allowance, and thermal load. | Typical commercial diameters may range from approximately 1 mm to more than 100 mm; define the exact nominal diameter and tolerance on the drawing. | Calibrated micrometer, optical measurement system, or coordinate measuring machine at multiple positions along the rod. | Specify measurement locations and temperature conditions. Diameter variation can affect sealing, heating uniformity, and mechanical fit. |
| Dimensional Tolerance | Diameter, length, straightness, and end geometry must be controlled according to the application. | A practical starting point for general-purpose rods is diameter tolerance of ±0.10 mm and length tolerance of ±1.0 mm, subject to drawing approval. | Inspection report based on calibrated instruments and a documented sampling plan. | Tighter tolerances may require additional grinding or polishing and should be priced separately. Avoid using “standard tolerance” without a numerical definition. |
| Length | Cut length must match the equipment design and allow for end finishing. | Define nominal length, permissible deviation, minimum usable length, and whether both ends require finishing. | Calibrated steel rule, height gauge, or optical comparator, depending on tolerance. | For international shipments, include protective end caps and specify whether quoted length is before or after end finishing. |
| Roundness and Straightness | Cross-section should remain circular and the rod should be free from visible bending. | Define maximum out-of-roundness and total indicator reading on the technical drawing; use application-specific limits rather than an undefined “round” description. | Rotational gauge measurement, laser measurement, or coordinate measurement over the full usable length. | Straightness is especially important for furnace elements, optical paths, guide components, and automated loading systems. |
| Surface Finish | Surface may be fire-polished, ground, or optically polished depending on function. | Define roughness or visual finish, for example polished, translucent, or ground; specify maximum scratches, pits, chips, and contamination. | Visual inspection under controlled lighting; profilometer measurement where a numerical roughness value is required. | A bright or transparent appearance alone does not prove a suitable surface finish. Use reference samples or approved visual standards for repeat orders. |
| Optical Transmission | Transmission range should correspond to ultraviolet, visible, near-infrared, or infrared service. | Define the wavelength range and minimum transmission only when optical performance is relevant; results must identify sample thickness and measurement conditions. | UV-Vis-NIR spectrophotometer or FTIR spectrometer, as appropriate to the specified wavelength range. | Transmission depends on hydroxyl content, impurities, bubbles, surface condition, and thickness. Do not accept an optical value without test conditions. |
| Hydroxyl Content | OH concentration must be controlled for applications involving ultraviolet transmission, infrared transmission, vacuum, or thermal cycling. | Set an application-specific maximum, commonly expressed in parts per million by mass or by an agreed spectroscopic classification. | Infrared spectroscopy or another validated supplier or third-party method. | Low-OH and high-OH fused silica behave differently during heating and in spectral transmission. State the required OH range explicitly. |
| Bubbles and Inclusions | Rod must be free from unacceptable bubbles, cords, stones, devitrification, and foreign inclusions. | Define maximum bubble size, total bubble count, inclusion type, and inspection zone; use zero-tolerance only where technically justified. | Visual inspection with transmitted and reflected light, supported by magnification or imaging when necessary. | Acceptance criteria should distinguish cosmetic marks from defects that can initiate fracture or distort optical and thermal performance. |
| Thermal Performance | Low thermal expansion and resistance to thermal shock are required for rapid heating and cooling. | Use a documented coefficient of thermal expansion requirement; fused silica is commonly specified at approximately 0.5 × 10⁻⁶ K−1 near room temperature, subject to grade and test range. | Dilatometry according to an agreed method and temperature range. | Never use a single expansion value without stating the temperature interval. Thermal shock performance also depends on geometry, surface defects, and heating rate. |
| Maximum Service Temperature | Operating temperature must be compatible with the rod geometry, load, atmosphere, and exposure duration. | Fused silica softening temperature is approximately 1,680°C, but continuous-use limits must be set below the softening range and validated for the specific design. | Review technical data and conduct application-specific thermal testing where continuous high-temperature service is critical. | High temperature can cause deformation, devitrification, or surface contamination even when the nominal softening temperature is not reached. |
| Mechanical Condition | Rod must withstand handling, machining, assembly, and expected service loads without unacceptable cracks or chips. | No through-cracks, harmful edge chips, or deep grinding damage; mechanical strength requirements should be defined by application and geometry. | Visual inspection, polarized-light stress inspection, and application-specific mechanical testing. | Quartz is brittle and surface flaws strongly influence strength. Specify handling controls and reject criteria for damage introduced after production. |
| Annealing and Internal Stress | Internal stress should be minimized through controlled thermal processing. | No visible abnormal birefringence or stress pattern under a suitable polarized-light inspection for components requiring thermal or mechanical stability. | Polariscopic inspection under documented lighting and viewing conditions. | Stress inspection is valuable for detecting processing problems that may not be visible under ordinary white light. |
| Cleanliness | Products must be free from oil, dust, abrasive residue, fingerprints, packaging fibers, and process chemicals. | Define allowable particulate level, cleaning chemistry, and whether cleanroom packaging is required. | Visual inspection, wipe testing, particle counting, or surface analysis according to end-use risk. | For vacuum, optical, laboratory, and semiconductor-related applications, cleanliness requirements should be written as a separate controlled specification. |
| End Finishing | Ends may be square-cut, chamfered, fire-polished, ground, or polished. | Specify end angle, chamfer width, edge sharpness, chip size, and allowable heat-affected zone. | Visual inspection and dimensional measurement using magnification where required. | Improper end finishing can create crack initiators and may interfere with seals, holders, or subsequent machining. |
| Packaging | Packaging must prevent impact, abrasion, moisture-related contamination, and movement during transport. | Individual sleeves or separators, cushioned inner packaging, rigid outer cartons or crates, and clear orientation markings for long rods. | Packaging inspection before dispatch and photographic evidence of packed goods. | Request shipment protection appropriate to the rod length and fragility. Packaging damage should be recorded before acceptance. |
| Traceability | Each shipment must be traceable to a production lot and inspection record. | Lot number, production date, material grade, quantity, inspection status, and certificate reference must appear on the packing list and product label. | Document review and label-to-certificate reconciliation. | Maintain traceability from purchase order through incoming inspection and final use. Mixed lots should not be accepted without prior approval. |
| Quality Management | Supplier should operate a documented quality-management system suitable for the risk and application. | Request evidence of a current ISO 9001-based quality system or an equivalent documented process; regulated applications may require additional sector controls. | Certificate review, supplier questionnaire, remote audit, or on-site audit. | Certification does not replace product inspection. Verify that the certified scope covers the relevant glass or quartz-processing activities. |
| Inspection Sampling | Incoming inspection should cover dimensions, appearance, documentation, and any critical chemical or optical properties. | Use a written sampling plan based on lot size, defect severity, supplier history, and application risk; critical defects should have zero acceptance where justified. | Inspection records using calibrated equipment and approved defect definitions. | Use tightened inspection for first articles, new suppliers, process changes, or repeated nonconformities, then adjust only with documented evidence. |
| Applicable Standards | Testing and quality requirements should reference recognized methods where available. | Potential references include ISO 9001 for quality management, ISO/IEC 17025 for testing-laboratory competence, ASTM E228 for thermal expansion, and ASTM E438 for laboratory glassware material classifications where applicable. | Confirm the latest applicable edition and ensure the selected method matches the product and intended use. | Standards should support the specification, not replace it. Always state the exact edition, test method, specimen condition, and acceptance limit in the purchase documentation. |
Global sourcing starts with supplier evidence, not a polished catalog. Quartz rods may look simple, yet purity, diameter, hydroxyl content, bubbles, and thermal history affect performance. Define the application first: lamp tubing, laboratory parts, semiconductor processing, or high-temperature insulation. Each use needs different tolerances. Ask for a technical drawing, inspection plan, sample lot, and certificate of analysis. Specify measurement methods, not only target values. That small detail prevents arguments later.
The U.S. Geological Survey’s Mineral Commodity Summaries 2025 reports approximately 97 million metric tons of U.S. industrial sand and gravel production in 2024. This figure concerns raw materials, not finished quartz rods. It signals supply depth, but never proves rod quality. The World Bank’s Logistics Performance Index 2023 assesses customs, infrastructure, shipment reliability, tracking, and delivery timeliness. Use these dimensions when comparing overseas suppliers. A lower quotation may hide weak packaging, port delays, or replacement costs.
Evaluate suppliers with a weighted scorecard. Give serious weight to dimensional consistency, traceability, testing capacity, and corrective-action records. Request recent batch data, not a perfect example from years ago. Arrange independent testing for purity, thermal shock resistance, and surface defects. Inspect cartons for foam separation, moisture barriers, and visible impact marks. Review export documents before payment milestones. A spreadsheet can look complete while one critical value is missing. I would still challenge my own scoring: supplier audits capture one day, while production changes every month. Keep retention samples from every accepted shipment and compare them against the original specification.
Recommended weighted criteria for identifying and evaluating international quartz rod suppliers. The weighting prioritizes technical conformity, quality assurance, traceability, and reliable delivery before price.
Use the 100-point model to compare qualified suppliers after reviewing material purity, dimensional tolerances, thermal performance, inspection records, production capacity, export documentation, and total landed cost.
Global quartz rod sourcing in 2026 starts with a like-for-like specification. Diameter, length, surface finish, bubble count, and hydroxyl content can change prices sharply. Public trade data rarely isolates quartz rods. The International Trade Centre places many shipments under wider glass categories. Therefore, compare three written quotations, not marketplace listings. Raw material is only one cost. Cutting, inspection, packaging, and breakage risk can alter landed pricing.
Ask suppliers for ISO 9001 records, material certificates, dimensional reports, and batch traceability. ISO 9001 confirms process control, not product quality. For laboratory testing, request reports from ISO/IEC 17025-accredited facilities. RoHS and REACH declarations may support European compliance, but they do not replace destination-specific checks. A useful inspection sample includes rod diameter, straightness, visible bubbles, and end squareness. Small omissions become expensive later.
Shipping needs more than a low freight quote. UNCTAD’s Review of Maritime Transport 2024 reported container transits through the Suez Canal falling about 67% during the disruption period. Rerouting can increase transit time, insurance, and inventory costs. Request both air and sea options, with shock-resistant tubes and moisture protection. Import duties depend on the final HS classification and destination. Use the official tariff database, verify customs valuation, and consider an advance classification ruling. I would not trust a duty estimate copied from a supplier email.
Global quartz rod sourcing requires more than comparing unit prices. Start with a controlled sample plan. Specify diameter tolerance, length, surface finish, hydroxyl content, purity, and thermal performance. Request three samples from each qualified supplier. Record packing condition, measured dimensions, and test results. In practice, one sample often looks excellent while the next exposes process variation. That is why repeatability matters more than a perfect first piece.
Inspection should combine supplier records with independent verification. Use calibrated instruments and retain photographs of every inspection batch. A contract should define acceptance limits, testing methods, replacement duties, payment milestones, and ownership of rejected goods. The World Bank’s Logistics Performance Index 2023 shows clear differences in customs, tracking, and delivery reliability across markets. Select routes using evidence, not assumptions. UNCTAD’s Review of Maritime Transport 2024 also reports that shipping carries over 80% of global merchandise trade by volume. Sea freight may reduce cost, but fragile rods need rigid tubes, moisture protection, and shock indicators.
Tips: Ask for a pre-shipment inspection before final payment. Add a small safety stock for critical dimensions. Keep two approved sources when qualification costs allow. Delivery dates still fail sometimes, even with good planning. I would not promise zero defects. A realistic contract manages that risk. Calibration certificates, lot traceability, and clear escalation contacts improve accountability. Recheck local import rules before dispatch, because documentation requirements can change.
Contact
KYOCERA SGS Precision Tools, Inc.
(330) 686-5700
150 Marc Drive
Cuyahoga Falls, OH 44223
Products
Resources